

SC 307
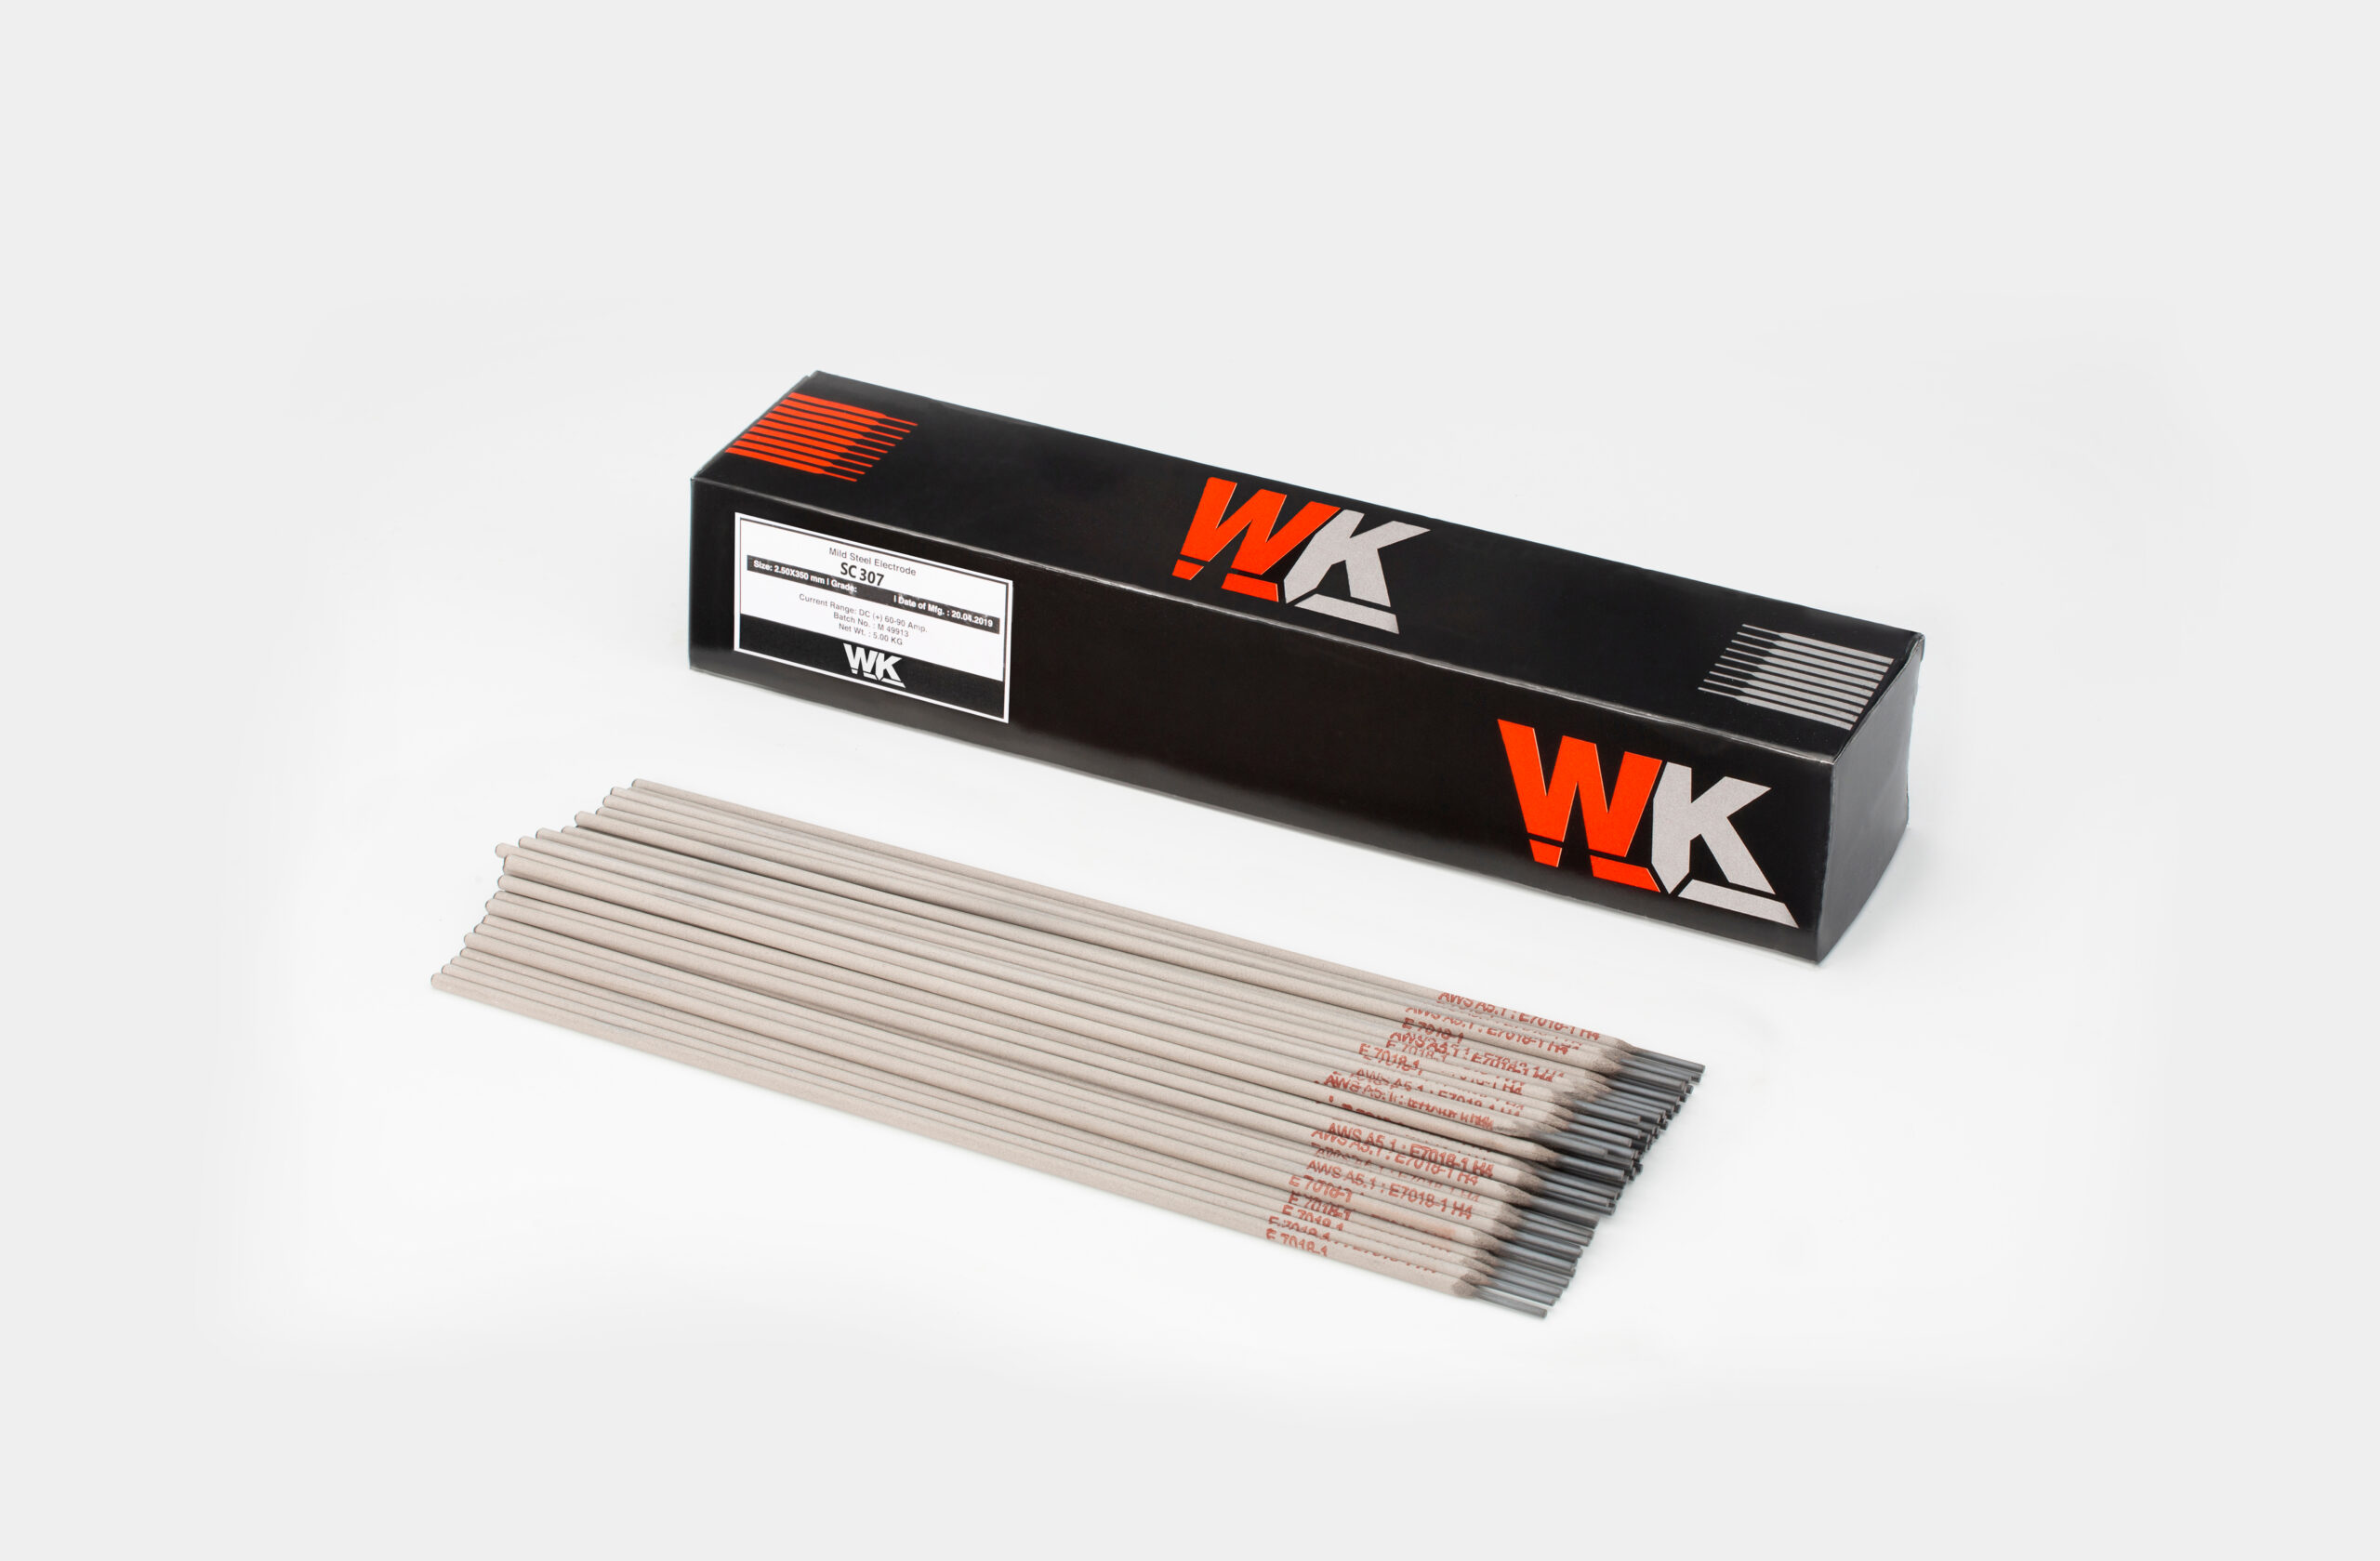
Austenitic (non-magnetic) rutile coated electrode for joining and overlaying on manganese steels(up to 14% Mn) and high sulphur and phosphorus containing steels
Repairing of pieces submitted to shocks or wear by friction. Excellent machinability, easy slag removal, nice aspect of the bead.

Related products
-
SFA T-50
Flux cored wire for all positions with excellent weldability characteristics. The SFA-T50 leaves a welding bead perfectly flat and with low spatter level. Designed for single-pass or multi-pass, the slag is easily removed and is prepared for use with Ar / CO2 (20-25%) or CO2 gas. It has excellent results in low temperature impact tests.
It is a flux cored wire of great efficiency thanks to its high deposition rate.
Extremely versatile for a wide variety of applications, such as shipbuilding, storage tanks, bridges and general fabrication of structural steels.
-
SC 7016
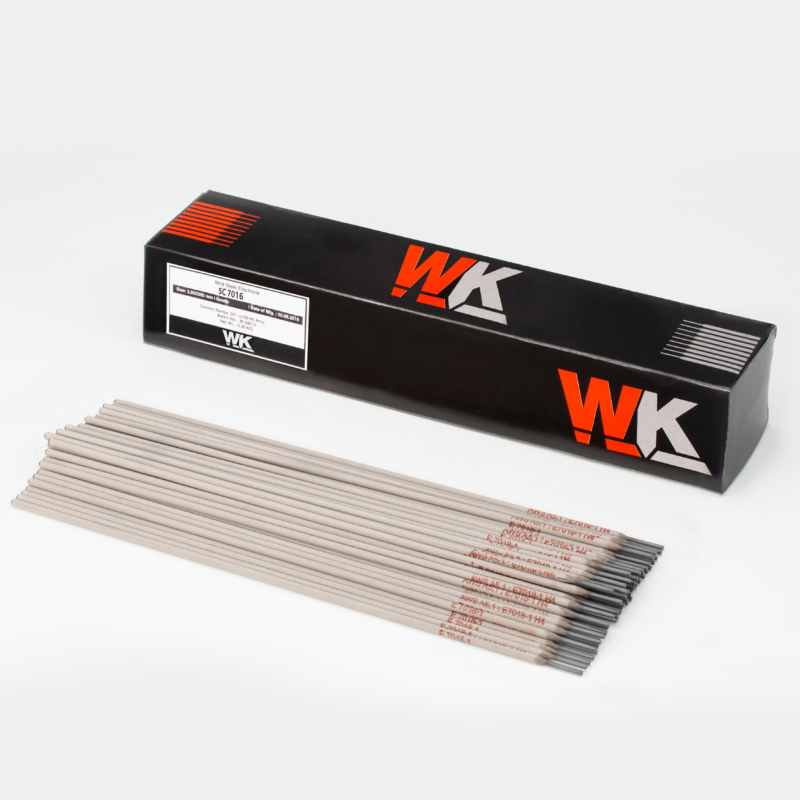
Basic coated, low hydrogen electrode for producing tough and crack-free welded joints. Good operating characteristics when positional welding.
-
SC 308L-17
Low carbon Rutile-silica-coated 19Cr, 10Ni austenitic stainless steel electrode with controlled ferrite approx 6-8% for maximum resistance to cracking and corrosion. Core wire is 308LER.